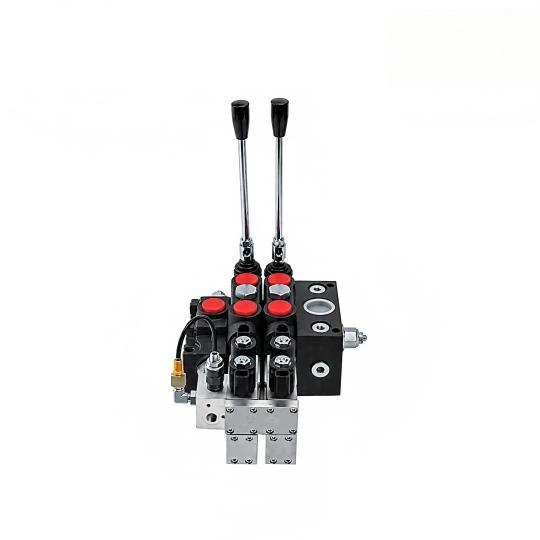
DCV200 Hydraulic Valve for Large Excavators & Systems
Product Overview
DCV200 sectional hydraulic valve is a heavy-duty high-flow modular hydraulic valve designed for large excavators and complex hydraulic systems. As a high-performance hydraulic valve, it accurately controls the flow, direction and pressure of hydraulic oil inside the hydraulic system, delivering synchronized, powerful multi-action operation for your Machine. Its sectional modular structure supports flexible spool configuration from 1 to 12 sections to meet sophisticated combined movements of large construction machinery.
Technical Specifications
- Rated flow: 200 L/min
- Max working pressure: 350 bar (5075 psi)
- Spool quantity: 1~12 sections, customizable
- Control modes: manual lever, cable remote, hydraulic control, electro-hydraulic proportional control
- Circuit type: parallel circuit / load sensing circuit optional
- Built-in components: main pressure relief valve, independent load check valve, anti-cavitation valve per section
- Operating temperature: -30℃ ~ +70℃
- Port thread: G, NPT, SAE thread optional
Working Principle
This hydraulic valve distributes pressurized hydraulic fluid from the hydraulic system to multiple actuators of the Machine. Each spool independently governs boom lifting, arm telescoping, bucket digging and slewing motions. The built-in load check valve locks loads reliably to prevent unexpected falling when the handle returns to neutral. Optional load-sensing technology automatically adjusts oil supply based on real-time load demand, cutting energy consumption and heat buildup within the hydraulic system during continuous heavy-duty operation.
Core Advantages
1. High-flow heavy-duty construction: 200L/min rated flow, capable of sustaining continuous heavy loads for large excavators.
2. Modular sectional design: easy to add or remove valve sections, simple for on-site maintenance and spare part replacement.
3. Precision machined spools: low internal leakage, smooth compound movements with little pressure shock during simultaneous actions.
4. Strong resistance to dust and vibration: robust cast valve body, stable performance in harsh construction site environments.
5. Comprehensive integrated safety: built-in relief and anti-cavitation valves protect the hydraulic system and machine components from overload and pressure spikes.
Application Range
Ideal for large excavators, mining excavators, material handlers, heavy-duty truck cranes and other large mobile Machine. Widely used in construction, quarrying, mining and large hydraulic system engineering projects.